Comparison tool-life record
550 parts/edgeCASE 16 / Machinery
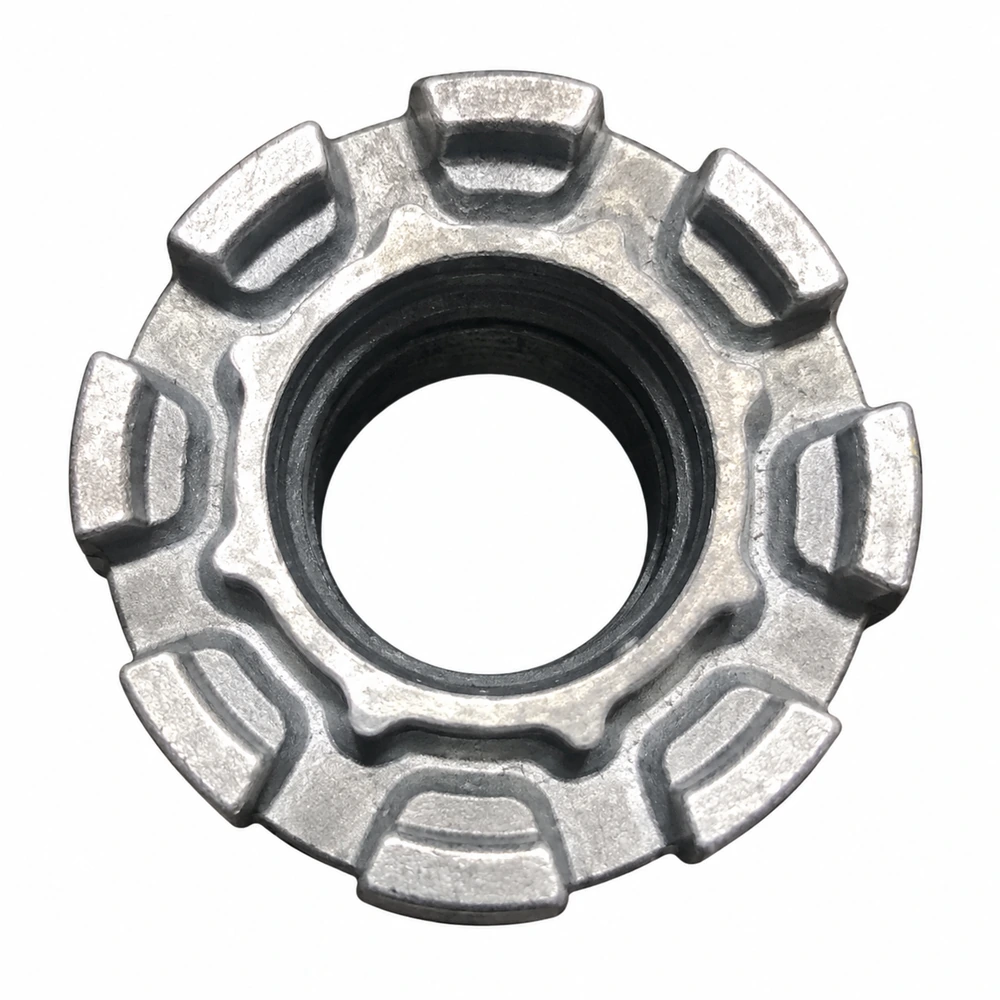
Face grooving of a powder metallurgy component
Application comparison using IKEN IKN1690 for heavily interrupted face grooving on a powder metallurgy component.
Workpiece and conditions
- Workpiece
- Powder metallurgy component
- Material
- Powder metallurgy material
- Hardness
- HRC50
- Machine type
- Automated production line
- Cooling
- Dry machining
- Operation
- Heavily interrupted face grooving
01 / TOOLING
Tooling
- IKEN tool
- IKGMN300-040-SFD IKN1690
- Previous tool
- MGMN300 (Imported)
Application objective
Extend tool life, reduce tool changes and optimize tooling cost per part.
02 / CUTTING CONDITIONS
Cutting conditions
- Cutting speed Vc
- 150 m/min
- Feed per revolution f
- 0.05 mm/rev
- Depth of cut ap (trial reference)
- 0.10 mm/pass
- Groove depth
- 2 mm
03 / APPLICATION RECORD
Recorded results
IKEN tool-life record
620 parts/edgeThe IKEN tool recorded a higher tool-life value than the comparison tool in this application.
Record notes
This case describes an application under the listed workpiece, tool and machining conditions. It does not guarantee tool life, cost or quality in other applications.
The source records a total groove depth of 2 mm, but no single-pass depth. The 0.10 mm/pass value is a trial starting reference, not an original tool-life test condition; confirm it for the setup, chip evacuation and actual trial cut.
Cost optimization is an application objective. The records do not include complete insert-price, machine-time and cost-per-part calculations, so no specific cost reduction is claimed.
Results apply to the workpiece and conditions recorded here. Tool life, surface quality and cycle time require validation for the actual material, machine, setup and parameters.